Buyers Guide for Hydraulic Safety Valves
A hydraulic safety valve protects equipment and personnel by relieving pressure when limits are exceeded. This guide covers selection criteria, ratings, body materials, and settings to help you choose the correct valve for your system.
- Match the valve maximum rated pressure to your system operating pressure with adequate margin.
- Confirm the set pressure and cracking pressure against your design limits and applicable standards.
- Choose body materials that resist your fluid, temperature, and corrosion environment.
- Verify that the valve type and port configuration fit your existing manifold or line layout.
- Keep a written record of the factory setting certificate and any field adjustments for traceability.
What is a hydraulic safety valve and why does it matter
A hydraulic safety valve is a pressure control device that opens automatically when the system pressure reaches a preset limit. It protects pumps, hoses, accumulators, and other components from overpressure conditions. In a typical installation, the valve sits in the return line or on a main line and directs excess fluid back to the reservoir.
The device differs from a pressure relief valve in how it responds to sudden pressure spikes. A relief valve modulates and closes as pressure falls, while a safety valve usually stays open until pressure drops below a defined recovery value. This difference affects system behavior during a blockage or pump failure. Selecting the wrong type can lead to valve chatter, short cycling, or inadequate protection.
Buyers often focus only on the set pressure. That is not enough. The valve must also fit the mechanical space, handle the fluid, and match the required response speed. A poor selection can force a retrofit or create a hidden failure point.
How to define the pressure requirements for your system
Start with the maximum working pressure of the circuit. This is the highest pressure the system is designed to handle under normal operation. The pump displacement, load requirements, and accumulator precharge all influence this value. A common practice is to set the safety valve at or slightly above the maximum working pressure.
For example, if the circuit operates at 250 bar and the pump is limited to that value, the safety valve might be set at 255 bar to 260 bar. This margin prevents nuisance opening during transients while still protecting the lines. If the system uses an accumulator, the maximum pressure may be higher. The valve set point should reflect the highest pressure the components can see.
Check the manufacturer data for the pump, hoses, and actuators. Each part has a maximum rated pressure. The safety valve must not exceed the lowest rating in the chain. If any component is rated lower, the system design needs review before buying a valve.
Document these values on the purchase order. A clear pressure specification prevents the vendor from guessing or defaulting to a standard size that does not fit.
Which valve type fits your application
The most common hydraulic safety valves are spring loaded. The spring sets the opening pressure. Other types include pilot operated valves, which use a lower pressure to trigger opening, and multi stage relief valves. The right type depends on the pressure range, required accuracy, and space constraints.
Spring loaded valves are standard for most industrial systems. They are compact, reliable, and available in many port configurations. Pilot operated valves are useful when the system pressure is high but the actuation pressure is low. They can open faster and are often used in high pressure circuits where a direct spring valve would be bulky.
Multi stage valves provide a two stage response. They crack at a lower pressure and fully open at a higher pressure. This is useful when you need to limit initial flow while allowing a larger flow rate at full opening. The type selection also depends on how the valve closes. Some are return to line, meaning they close when pressure drops. Others are pilot operated and require an external signal to close.
Match the valve type to the failure mode you are protecting against. A pump cavitation event, a hose burst, or a blocked actuator each create different pressure profiles. The valve response must match that profile.
What materials and finishes should you specify
The body material must match the fluid and environment. Steel bodies are common for standard mineral oil systems. Stainless steel bodies are specified when the fluid is corrosive or when the valve is exposed to moisture, salt, or chemical cleaning. The internal seals are often made from nitrile rubber or PTFE. Choose the seal material based on the fluid temperature and chemical compatibility.
Consider the finish. A nickel chrome or similar plating protects against corrosion and wear. In food processing, pharmaceutical, or marine applications, the finish may need to meet specific cleanliness or corrosion standards. The finish also affects the life of the internal components. A poor finish can rust and contaminate the fluid.
Check the port threads and fittings. The standard is usually a metric or UNF thread, but the specific size must match your manifold or line. If the valve is installed in a manifold, the port orientation and depth matter. A valve that does not seat correctly can leak or fail to close. Specify the thread size, thread depth, and any required adapter in the order.
How to evaluate the set pressure and cracking pressure
The set pressure is the pressure at which the valve fully opens. The cracking pressure is the pressure at which the valve begins to open. For many safety valves, the cracking pressure is lower than the set pressure. The difference is called the hysteresis or the pressure drop. A typical hysteresis might be a few percent of the set pressure, depending on the design.
When selecting a valve, specify both values if the application requires it. For example, if the system must not exceed 300 bar, the set pressure should be at or below 300 bar. The cracking pressure should be high enough to avoid nuisance opening during normal operation. If the cracking pressure is too low, the valve will cycle and wear out quickly.
The manufacturer usually provides a test certificate that lists the set pressure and cracking pressure. This document is critical for safety and maintenance records. Keep it with the valve. If the valve is adjusted in the field, record the new setting and the date. An unrecorded adjustment can invalidate the safety case.
How to check the flow and response characteristics
The valve must handle the maximum flow that can reach it. In a pump failure or hose burst, the flow can be much higher than normal operating flow. The valve orifice size determines how much flow it can pass. A valve that is too small will not reduce pressure quickly enough. A valve that is too large may open too early or chatter.
The response time is the time between the pressure spike and full opening. For high speed systems, a fast response is needed. Pilot operated valves often open faster than direct spring valves. The response time depends on the valve size, the set pressure, and the system dynamics. If the valve opens too slowly, the pressure can exceed the set point before the valve fully opens.
Specify the maximum flow rate in the purchase order. The manufacturer can confirm whether the selected valve meets that requirement. If the flow is uncertain, choose a valve with a larger orifice or a pilot operated design. This gives more margin and reduces the risk of overpressure.
What standards and documentation should you require
Hydraulic safety valves are often built to recognized standards. These standards define the test methods, pressure ratings, and performance requirements. The specific standard depends on the region and application. For industrial hydraulics, common standards cover design, testing, and safety.
Require the manufacturer to state the applicable standard on the data sheet. Also ask for the test certificate that proves the valve was tested at the set pressure. For safety critical applications, a third party certification may be required. The documentation should include the set pressure, cracking pressure, flow rating, and any deviations from the standard.
Keep these documents with the maintenance records. If the valve fails or if a safety incident occurs, the test certificate shows that the valve was set and tested correctly. It also supports the maintenance schedule. Without it, the valve is just a part in a system with no traceability.
Criteria table for evaluating hydraulic safety valves
| Criterion | What to look for | Why it matters |
|---|---|---|
| Set pressure | Matches or exceeds system maximum working pressure with margin | Prevents overpressure while avoiding nuisance opening |
| Cracking pressure | Higher than normal operating pressure to prevent cycling | Reduces wear and extends valve life |
| Body material | Compatible with fluid and environment, such as steel or stainless | Prevents corrosion and contamination |
| Flow capacity | Rated for maximum expected flow during a failure event | Ensures pressure drops quickly enough |
| Port configuration | Matches manifold or line thread size and orientation | Prevents leaks and installation errors |
| Test certificate | Lists set and cracking pressure with standard reference | Provides traceability and safety records |
| Response time | Fast enough for the system pressure spike profile | Protects components from exceeding limits |
Decision checklist before you place the order
- Confirm the maximum working pressure and the highest pressure any component can see.
- Choose the valve type, such as spring loaded or pilot operated, based on the failure mode.
- Specify the set pressure and cracking pressure in writing.
- Select the body material and finish for the fluid and environment.
- Verify the flow capacity for the worst case flow scenario.
- Match the port size and thread to the installation.
- Require the test certificate and the applicable standard on the data sheet.
- Keep a copy of the order and the certificate with the maintenance records.
This checklist ensures that the valve is selected for function, not just for the label on the box. A valve that is set correctly but installed wrong will fail. A valve that is the right size but the wrong type will not protect the system. The selection is a design decision, not a purchase order item.
Common selection mistakes to avoid
A common mistake is to choose the largest valve available. Bigger is not always better. A larger orifice may open too early or cause pressure spikes when it closes. It also costs more and may not fit the manifold.
Another mistake is to ignore the fluid temperature. A valve designed for 60 degrees Celsius may not perform well at 90 degrees. The spring rate changes with temperature, and the set pressure can drift. Specify the operating temperature range.
Do not assume that any relief valve will work as a safety valve. The response characteristics are different. A relief valve may modulate and close, while a safety valve stays open. Using a relief valve where a safety valve is required can leave the system unprotected during a blockage.
Finally, do not adjust the valve without documentation. A field adjustment changes the set point. If it is not recorded, the next technician will not know the correct value. This can lead to a valve that is set too low, causing constant cycling, or too high, leaving the system exposed.
How to verify the valve after installation
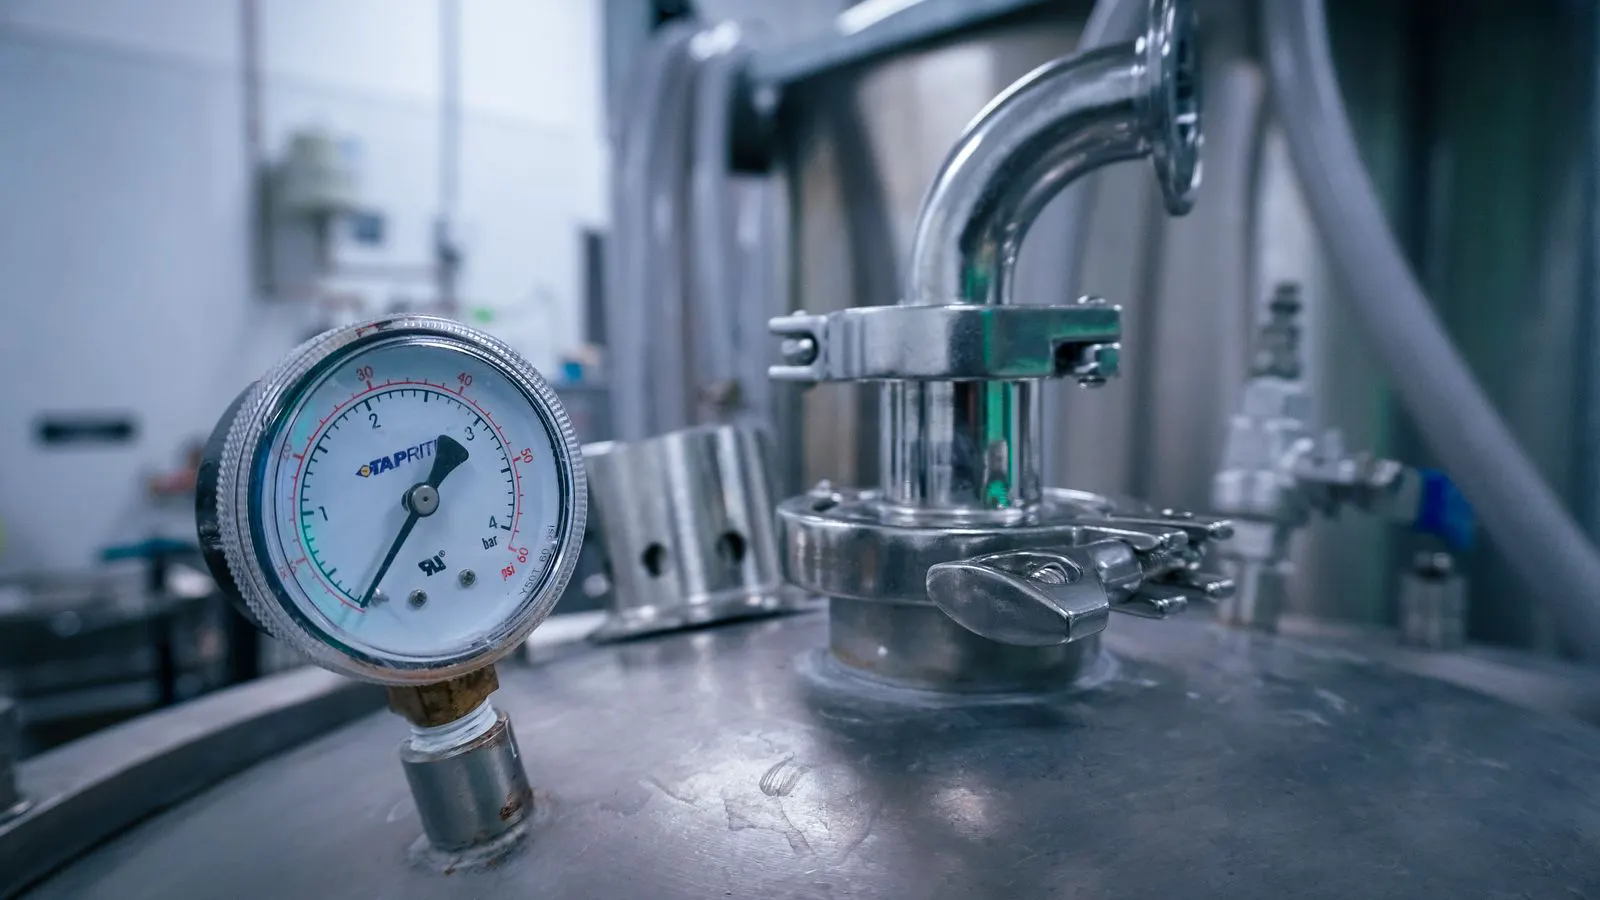
After the valve is installed, check the set pressure with a calibrated gauge. Connect the gauge to the valve inlet and slowly increase the pressure. The valve should open at the set pressure and close at the recovery pressure. Record the values.
Check for leaks at the ports and the body. A leak can indicate a damaged seal or a cross threaded fitting. Also check the flow direction. The valve should only open in the correct direction. If it opens in reverse, the system is not protected.
Monitor the system for a few operating cycles. Watch for valve chatter or short cycling. If the valve opens and closes repeatedly, the set pressure is too close to the operating pressure. Adjust the set pressure upward or review the system design.
Keep the test results with the maintenance log. This provides a baseline for future checks. If the valve starts to open at a lower pressure than it did when installed, the spring may be fatigued or the seat may be worn. Replace the valve before it fails in the field.
Frequently asked questions
What is the difference between a hydraulic safety valve and a pressure relief valve?
A pressure relief valve modulates and closes as pressure falls. A safety valve typically stays open until pressure drops below a recovery value. The response difference affects how the system behaves during overpressure events.
How do I know what set pressure to specify?
Set the valve at or slightly above the maximum working pressure of the circuit. Check the ratings of all components in the chain. The set pressure must not exceed the lowest rating.
Can I use a standard relief valve as a safety valve?
Not always. The response characteristics are different. A relief valve may modulate and close, while a safety valve stays open. Verify the valve type matches the required protection.
What documents should I keep with the valve?
Keep the test certificate, the data sheet with the applicable standard, and any field adjustment records. These documents provide traceability and support maintenance.
What if the valve chatters after installation?
Chattering usually means the set pressure is too close to the operating pressure. Check the set pressure with a calibrated gauge. Adjust the set pressure upward or review the system design. ===END===